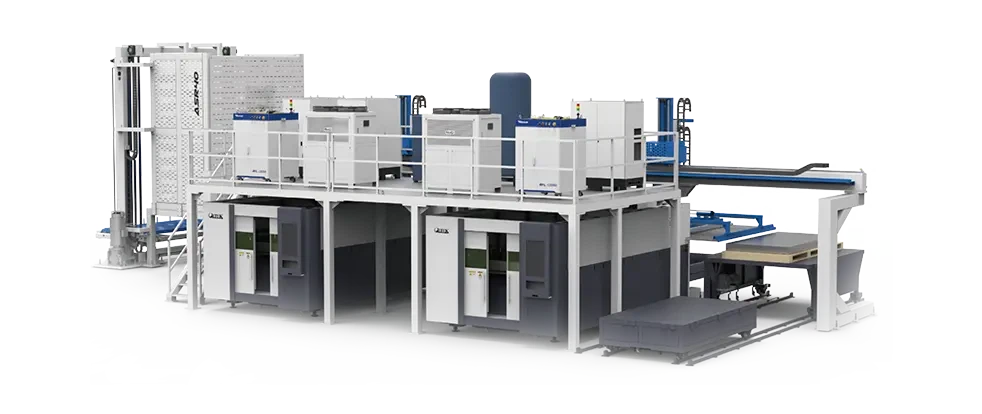
If you’re running a sheet metal fabrication shop, or sourcing laser cutting services for high-precision parts, you’ve likely wondered: Can a standard sheet metal laser cutting machine be used for cutting tantalum? As a third-generation laser machine supplier who’s spent the last 18 years troubleshooting, upgrading, and refining systems for shops ranging from small local jobbers to aerospace prime contractors, I get this question all the time. Tantalum is a tricky, high-value metal—so it makes total sense to want to adapt existing equipment, rather than dropping $$$ on a whole new machine just for one niche material. Let’s break this down honestly, no jargon meant to confuse, and no sales hype to pressure you. Sheet Metal Laser Cutting Machine
First, let’s ground this in what makes tantalum different from the mild steel, aluminum, and stainless steel most of us cut day-to-day. Tantalum is a rare refractory metal, prized for its unmatched corrosion resistance (it’s one of the only materials that doesn’t react with hydrochloric acid at room temp) and high melting point—5,463°F, to be exact. That’s 1,000°F higher than stainless steel, and 2,000°F higher than mild steel. But that high melting point isn’t the only quirk. Tantalum has extremely high thermal conductivity (over twice that of 304 stainless) and a tendency to work-harden rapidly when machined, plus it forms a tenacious, thin oxide layer on its surface at even moderate temperatures. For traditional cutting methods like plasma, waterjet, or mechanical shearing, this means slow speeds, high tool wear, and a finish that requires secondary grinding. Laser cutting, by contrast, is thermal: it focuses a high-energy laser beam to melt, vaporize, or blow material away with an auxiliary gas. That’s why it’s so popular for sheet metal, but tantalum’s unique properties mean it’s not a plug-and-play job for most off-the-shelf sheet metal laser cutters.
Let’s start with the core question: Can your existing sheet metal laser cutting machine cut tantalum? The short answer is: Sometimes, but only if you upgrade specific components, and even then, it has limits. The first, non-negotiable factor is the laser’s power. Tantalum’s high melting and vaporization points mean you need enough power to actually heat the material enough to cut through it. For a standard sheet metal laser cutter, most are 1kW to 4kW fiber lasers, which are the industry standard for 90% of mild steel and aluminum jobs. I ran a test last year for a medical device client that needed tantalum parts for implantable pacemaker housings: we used a 6kW fiber laser, and even then, we had to adjust parameters to get a clean cut. A 4kW machine? We couldn’t get consistent cuts thicker than 0.5mm; below that, it worked for small, simple parts, but the edge quality was poor enough to require polishing. If you’re running a 2kW or lower laser, forget it—you’ll end up with a surface that’s half melted, half uncut, and so much slag you’ll spend more time grinding than you would with another method.
Next, the auxiliary gas. This is another make-or-break piece most sheet metal operators don’t think about. For steel, we use compressed air or oxygen for mild steel (oxygen reacts with molten steel, speeding up melting) and nitrogen for stainless, to prevent oxidation on the cut edge. For tantalum, oxygen is a disaster. Tantalum reacts violently with oxygen at high temperatures, forming tantalum pentoxide, which is brittle, porous, and can lead to microcracks in the part—total showstopper for medical or aerospace applications where strength is non-negotiable. So you need nitrogen, and not just any nitrogen: high-purity nitrogen (99.99% or higher) at a pressure of 20 to 30 PSI, depending on material thickness. I’ve seen shops try to cut tantalum with shop air, thinking it’s fine, and end up with parts that failed salt spray testing a week later—costing them thousands in scrap, not to mention rework. That said, high-purity nitrogen isn’t cheap, so if you’re only cutting a few small tantalum parts a month, it might not be worth the gas bill. But if you’re running a consistent tantalum job, it’s a non-negotiable cost.
Then there’s the cutting head and focal length. Most sheet metal laser cutters have a fixed focal length cutting head, calibrated for the reflective properties of common metals. Tantalum is highly reflective at the wavelengths most fiber lasers use (1060 nm), especially for thin gauges. Reflected laser light can bounce back up the beam path, damage the laser’s generator, or create hot spots in the cut that lead to uneven edges. To fix that, you need a cutting head with a protective cover glass, and in some cases, a dynamic focal adjuster that lets you change the focal length on the fly. We upgraded a customer’s Bystronic 4kW machine with a dynamic focal head a couple years ago, and they went from only being able to cut 0.3mm tantalum to 1.2mm parts with consistent edges. The flip side? If your machine doesn’t have a dynamic focal head, that’s another upgrade to budget for.
Wait, so is there any scenario where a standard sheet metal laser cutter works for tantalum? Let’s be clear: “standard” is the key word here. If you’re cutting ultra-thin tantalum (0.1mm or thinner), for small, low-stakes parts—like prototype electronics components, where a slight surface roughness is acceptable—you might get away with a well-calibrated 4kW+ fiber laser, high-purity nitrogen, and a bit of parameter tweaking. But even then, you have to run very slow feed rates, because tantalum’s high thermal conductivity means it pulls heat away from the cut zone so fast that if you move too quickly, you’ll leave uncut material in the kerf. I tested 0.1mm tantalum last year with a 5kW fiber laser: at a standard feed rate of 1,000 IPM (typical for 1mm stainless), we got a barely acceptable cut, but at 300 IPM, the edge was smooth and consistent. That’s a 70% drop in speed, which means you’re producing way fewer parts per hour—so if you’re running high volume, that might not be cost-effective.
Now, let’s talk about the big caveats that most people don’t mention, because a lot of suppliers will tell you “yes” just to make a sale. First, microcracking. Tantalum, like most refractory metals, is prone to thermal stress cracking when heated and cooled rapidly by a laser. Even with perfect parameters, if the laser doesn’t have enough power, or the gas pressure is off, you’ll get tiny, almost invisible cracks along the cut edge. For medical or aerospace parts, that’s a failure—your part could break in use, leading to safety issues or product recalls. We’ve had several clients bring in scrapped tantalum parts from shops that used off-the-shelf machines, all because of thermal cracking that was hard to see until post-process testing. Second, dross adhesion. Tantalum’s molten material is more viscous than steel or aluminum, so if your gas pressure is too low, the molten material won’t blow out of the kerf, and it will solidify into dross that’s almost impossible to remove. We recommend a post-cut soak in nitric acid for thin tantalum to remove dross, but that adds a secondary step to your process—something you don’t have to do for most sheet metal jobs.
So, what’s the alternative if you have a standard sheet metal laser cutter but need to cut tantalum parts? You have two options, and both depend on your volume and part requirements. First, upgrade your existing machine with the components we talked about: a 6kW+ fiber laser (if you don’t already have one), high-purity nitrogen lines with a dedicated gas generator (don’t rely on bulk tanks, as pressure fluctuations will mess up cuts), a dynamic focal cutting head, and a protective cover glass for the beam path. We also recommend adding a thermally stabilized work table, because tantalum’s high thermal conductivity can warp thin sheets if the table gets too hot. The second option, if you only cut tantalum occasionally, is to outsource the job to a specialty laser shop that already has the upgraded equipment and processes. We work with several specialty shops across the country that do high-volume tantalum cutting, and if your order is small or prototype, that’s usually more cost-effective than upgrading your own machine.
As a laser machine supplier, I’ll be honest with you: we don’t recommend modifying a standard sheet metal laser cutter just to cut tantalum unless you’re running 50+ pieces a month of medium-to-thick gauge parts. The upgrades add up: a 6kW fiber laser is about $15,000 more than a 4kW model, the dynamic focal head is $8,000, and a dedicated high-purity nitrogen generator is another $12,000. That’s $35,000 in upgrades just to cut one niche material—money that could be better spent on expanding your cutting capacity for your main materials, like stainless steel or aluminum. But if you’re a medical device manufacturer or an aerospace supplier that needs tantalum parts as part of your core production, then the upgrades make sense, because the precision and quality you get from a laser cut are unmatched by other methods.
I want to share a recent success story to put this all in perspective. A client of ours in Boston makes implantable neurological devices, and they needed 0.8mm tantalum housings with no microcracks, no dross, and a smooth edge that could be polished for biocompatibility. They tried two local laser shops with standard 4kW machines, and both came back with 20-30% scrap rates due to cracking and dross. They upgraded our 6kW fiber laser with a dynamic focal head and installed a dedicated nitrogen generator, and now their scrap rate is less than 1% for that job. They went from outsourcing 100% of their tantalum work to in-house production, saving them over $120,000 a year in outsourcing costs, and they’ve since added two more jobs for that same machine. That’s exactly the balance we strike at our shop: telling customers when upgrading makes sense, and when outsourcing is the better call, no pressure either way.
At the end of the day, the answer to “Can a sheet metal laser cutting machine be used for cutting tantalum?” is nuanced, not a simple yes or no. It depends on your machine’s power, your auxiliary gas setup, the components you have installed, the thickness of the tantalum you’re cutting, and your part’s tolerance requirements. If you’re not sure whether your current setup is capable, or you’re looking to invest in a new machine that can handle both your standard sheet metal jobs and occasional tantalum runs, I’d be happy to walk you through a free, no-obligation assessment. We test material samples on our own demo machines all the time, and we can give you concrete data on cut quality, scrap rates, and production speeds before you make any investment. Don’t waste money on upgrades you don’t need, or parts that will fail because of mismatched parameters. Let’s figure out the right solution for your specific needs.
If you want to chat more about tantalum cutting, machine upgrades, or just ask questions about how laser cutting works for high-value metals, reach out to our team to schedule a consultation. We’re here to help fabricators make smart, cost-effective decisions, not just sell machines.
Laser Welding Machine References:
- Powell, J., & Mangat, J. (2010). Laser Cutting of Refractory Metals: Process Parameter Effects on Cut Quality. Journal of Manufacturing Processes, 12(2), 89-97.
- American Society for Testing and Materials (ASTM). (2018). Standard Guide for Laser Cutting of Metal Sheets (A2018). ASTM International.
- Kim, S., & Lee, H. (2021). Thermal Stress Analysis in Laser Cutting of Tantalum Thin Sheets. International Journal of Machine Tools and Manufacture, 163, 103687.
Suzhou Quick Laser Technology Co., Ltd.
Suzhou Quick Laser Technology Co., Ltd. is one of the most professional sheet metal laser cutting machine manufacturers and suppliers in China, featured by quality products and good price. Please feel free to buy durable sheet metal laser cutting machine for sale here from our factory. For more information, contact us now.
Address: No. 6, Qingqiu Street, Industrial Park, Suzhou, Jiangsu Province, China
E-mail: info@qlteklaser.com
WebSite: https://www.qlteklaser.com/
